Casting Line
HART Design & Manufacturing’s Casting Machines can be configured for Slice-on-Slice (SOS) cheese production, Direct Shred applications, or both with changeover.
HART Casting Machine Features:
- Two Stainless Steel Conveyor Belts
- Assorted Scrapers & Cheese Sheet Transitioning Components
- Cooling Pan System (for optimal sheet casting & forming)
- Optional Additional Thermal Transfer Zones (for localized heating/cooling)
- Cheese Supply: HART Hopper Pump Assembly (provides continuous supply of cheese for casting)
- Process Cheese Infeed: Patented Adjustable Manifold for Process Cheese
- Pasta Filata Infeed: Nozzle & Forming Roller Infeed System for Pasta Filata Cheeses like Mozzarella
- SOS Output: Slitter Assembly (ribbon cutting) and Twist & Stack (ribbon stacking) directly onto a Transfer Conveyor (receives stacked ribbons)
- Direct Shred Output: Slitter Assembly (split sheet) and directly feed a HART Dicer Shredder
Reliably Handle Process Cheese up to 11,000 lbs/hr
For Slice-on-Slice production, HART’s Casting Lines can incorporate a Servo Cutoff to cut stacked cheese ribbons into loaves at programmed lengths. Hopper Pump Skids automate the receiving of cheese batches from upstream processing and allow for HMI-controlled loaf weight adjustments while maintaining a consistent cheese supply. Additional downstream equipment, including Stackers, AutoHarps and Wrapping equipment can be integrated based on production requirements.
After the desired uniform cheese sheet thickness is obtained by adjusting the manifold valves and thickness bar, weight control is accomplished by varying the cheese pump speed.
Once the cheese sheet reaches the opposite end of the conveyor, the sheet is directed around the end drum, over the doctor blade and onto the lower stainless steel belt. After the sheet passes over the lower belt and is slit into ribbons, the ribbons are directed over transfer rolls and through the twist and stack section.
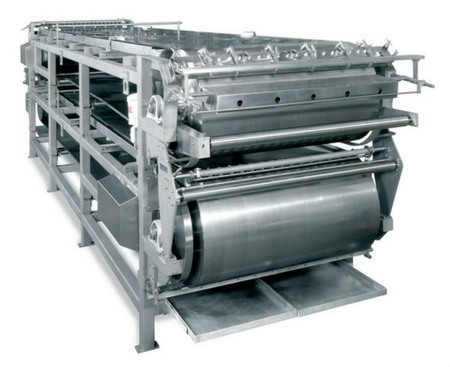
Cooling of the casting line is accomplished with cooling pans: there are usually two underneath the top belt and two underneath the lower belt. As the stainless steel conveyor belt passes over the cooling pans, coolant or chilled water is pumped into the pans and cools the belt, which in turn cools the cheese. By adjusting the flow pumped into the cooling pans, one can adjust the cooling rate of the product.
Casting Line Features
-
- Endless stainless steel product belts with bottom mounted v-belt for tracking
- Stainless steel drums for product belt drive
- HART’s patented drum mounted adjustable width manifold
- Stainless steel cooling pans with manifold spray pipes
- Quick-change sanitary slitter assembly
- Ribbon stacking unit with offset stacking feature
- Stainless steel operator enclosure with master speed control
- Designed and built to USDA standards
- NEMA 4x stainless steel enclosures
- Sanitary stainless steel sanitary frame construction
- Stainless steel casting line cooling pan plumbing
- Stainless steel sanitary electrostatic lecithin application system includes spray system and air/humidity management designed to maintain 50% or less humidity in the oiling canopy.
- Manifold infeed sanitary inlet piping
- Manifold hoist mast
- Manifold hoist (mounts to manifold hoist mast manual chain operation)
- Stainless steel belt
- Stainless steel sanitary bearing housings and heavy duty bearing inserts
- Stainless steel sanitary motors, drives, and components
- USDA inspected and approved
- PLC controls with PanelView touchscreen
- Numerous lengths and width to accommodate a wide variety of products (1,100 lbs/hr to 11,000 lbs/hr)
- Inner glycol pan is fully covered by product belt to further control cooling media and minimize exposed glycol
- Cooling with glycol or chilled fresh water
- Triple wiper system in cooling pans
- Ability to run various processed cheese as well as mozzarella
- Quick-change doctor wire/blade holder
- Quick-change from inside lane to outside lane when multiple casting lines are used
- Integral stainless steel guarding with sight holes
-
Closed-loop cooling system to eliminate any chance of glycol leakage
-
Cutoff / Manifold / Checkweigher weight adjustment through complete feedback loop with adjustment (various levels of automation)
-
Automatic belt tensioning system to increase product belt longevity and tracking